Plant air that never
stops the line
Actuation, conveying, cleaning, air boost — production machinery assumes compressed air is simply there. The plant behind it decides whether it is efficient or expensive.
Air is a utility here. Downtime is not.
Factory air at a glance
The four constraints that shape every plant room.
What a production hall asks of an air system
Stability first, then the cost of every cubic metre.
A.The line
Cylinders, valves and conveying systems need pressure that holds while demand swings across shifts. Dryer and filtration are matched to the air-quality class the process requires — moisture or oil carryover shows up downstream as rejects.
B.The economics
Electricity is most of an air system’s lifetime cost. Specific power (kW per m³/min), part-load control and heat recovery decide the running bill — which is why machine-hall projects start from consumption data, not nameplate.
Recommended SIND equipment
The two product families factories standardise on.
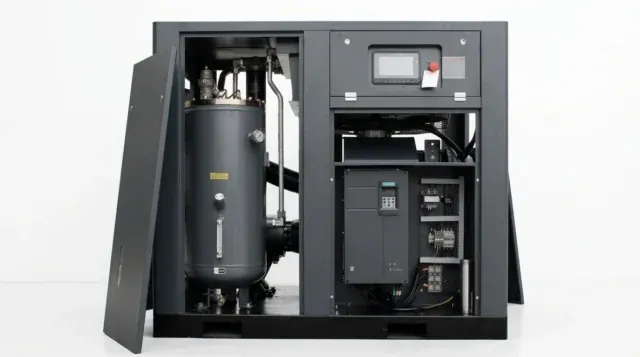
Oil-Lubricated Screw Compressors
Fixed-speed and VPM screw units from 7.5 to 400 kW — the efficient base load for general plant air.
View the range →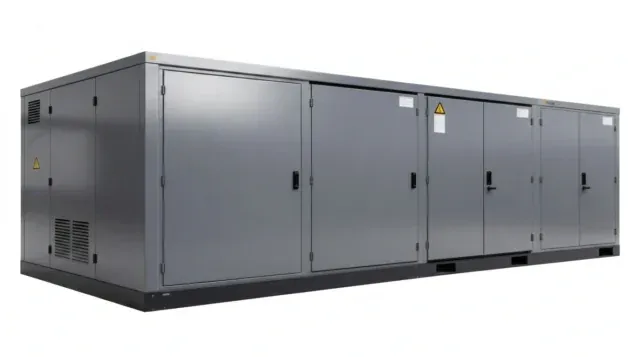
Integrated Compressor Stations
Compressor, storage and treatment engineered as one delivered station — from 20 m³/min class upward.
View the range →Six checks that keep a plant quote accurate
- Shift demand profile — base load versus peaks
- Pressure each machine actually needs, per branch
- Air-quality class: dew point and oil content
- Specific power target and part-load control
- Compressor room ventilation and floor plan
- Redundancy for lines that cannot stop
What does plant air cost per year?
Electricity is the largest line item — estimate it before you compare machines.
Indicative energy arithmetic, not a performance promise. Your real figure depends on load profile, pressure band and site power quality — send consumption data and we will model the upgrade path.
Request an energy review